Product Description
A
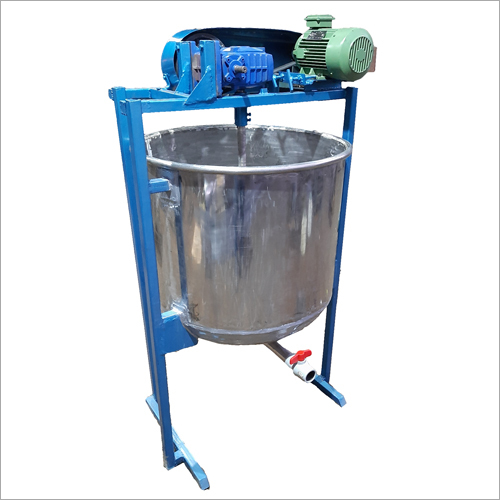
jacketed reactor is a type of chemical reactor that utilizes a jacket around the main reaction chamber to control the temperature of the reaction. The jacket is filled with a heat transfer medium, such as water or oil, which is circulated through the jacket to provide either heating or cooling of the reaction. This type of reactor is commonly used in the production of pharmaceuticals, chemicals, and food products.
Unmatched Versatility and PerformanceWith a wide range of capacity options and customizable features including agitator type, lining, pressure, and temperature specifications, this jacketed reactor addresses complex process requirements. Choose between SS Ball or Butterfly discharge valves, various surface finishes, and nozzle connection types to precisely match your operational needs.
Superior Design & ComplianceManufactured to highest industry standards, the reactor can be tailored for GMP, ASME, or CE compliance. Optional features such as double mechanical seals, PLC controls, and clean-in-place systems ensure safe, reliable and flexible operation for pharmaceutical, chemical, and food processing environments.
FAQ's of Jacketed Reactor:
Q: How does the optional insulation benefit jacketed reactor operations?
A: Optional insulation, such as mineral wool or glass wool, helps minimize heat loss and improves thermal efficiency by keeping the process temperature stable. This leads to lower energy consumption and more precise control over reaction conditions.
Q: What is the maximum internal pressure and working temperature the reactor can handle?
A: The jacketed reactor is engineered to withstand internal pressures of up to 6 bar, with custom designs available for pressures up to 10 bar. It can safely operate at temperatures up to 250C, supporting applications that require rigorous thermal conditions.
Q: Where can this jacketed reactor be used?
A: This reactor is suitable for chemical, pharmaceutical, and food processing industries. Its robust design ensures safe handling of corrosive materials and high-pressure reactions, making it ideal for batch processing, mixing, and synthesis tasks.
Q: What process controls and automation options are available?
A: The reactor can be supplied with automated operations and PLC controls, allowing for programmable settings and precise process management. This enhances repeatability, safety, and ease of monitoring during production runs.
Q: What are the benefits of variable agitator speed and multiple mixer types?
A: Variable agitator speeds ranging from 20 to 75 RPM allow for optimized mixing of diverse substances, while selectable mixer types-agitator, anchor, or turbine-ensure effective blending and transfer of heat throughout the vessel, improving product homogeneity and process efficiency.
Q: How does the cleaning process work for this reactor?
A: A Clean-In-Place (CIP) system is optionally available, enabling thorough cleaning without disassembling the reactor. This ensures faster turnaround, maintains product purity, and helps meet stringent regulatory requirements in sensitive industries.






 Send Inquiry


 Send Inquiry
 Send SMS
 Call Me Free


